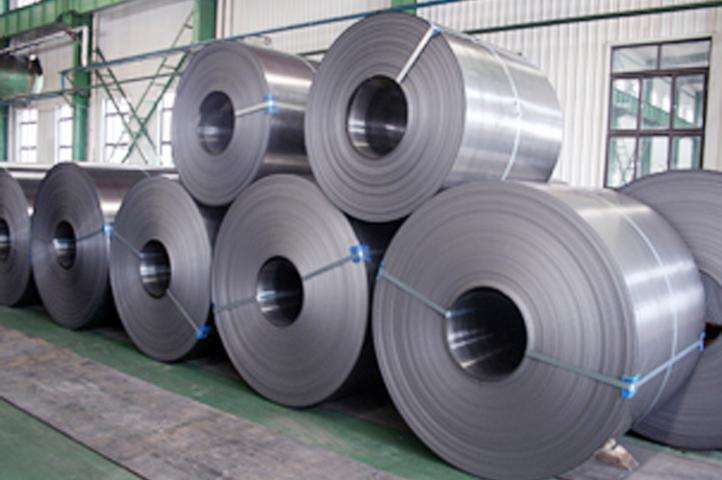
The production process of cold rolled coil is slightly different
according to the variety and specification of raw materials and
products. The general process of cold rolled steel coil is introduced as
follows.
1.Pickling.A continuous pickling unit is used to
remove the surface iron oxide scale of hot rolled coil.Acid is now
mostly hydrochloric acid.Before pickling, first process is welding and
rolling, some also go through continuous "black annealing".After
pickling, the next processes are wash, dry, trim and roll.
2.Cold rolling.After the pickling, the strip billet is rolled to the
thickness of the finished product on the cold rolling mill, generally
without intermediate annealing.The total compression rate of cold
rolling of five-stand tandem mill is generally 60 ~ 80%, mainly rolling
automobile plate, enamel plate and galvanized plate with thickness of
0.3 ~ 3mm.Six stand tandem mill is mainly used to roll tin-plated sheet
with a thickness of 0.15 ~ 0.5mm, and the total compression rate of cold
rolling is generally 70 ~ 90%.
3. Annealing.The purpose of
annealing is to eliminate cold rolling hardening and to make the steel
plate recrystallized and softened with good plasticity.The annealing
method is coil annealing with cover furnace and continuous annealing
with continuous furnace.Coil annealing is divided into tight coil
annealing and loose coil annealing.Continuous furnace annealing is
divided into vertical continuous furnace annealing and horizontal
continuous furnace annealing.Protective gases are generally introduced
into the furnace.At present, most of them adopt cover furnace annealing,
because of flexible and saving investment.
4.Leveling.The
purpose of leveling is to avoid plastic instability and improve the
quality (flatness and surface condition) of the annealed steel sheet
during stamping.There are two kinds of leveling mill, single stand
reversible and double stand, and the leveling compression rate is 0.5 ~
4%.Double stand rolling mill with high efficiency and high compression
rate can be used for secondary cold rolling and further rolling of thin
steel sheet.If cooperate with five stand continuous rolling mill, can
produce 0.10 ~ 0.15mm coating, shearing and packaging need coating steel
plate sent to galvanized, tin or organic coating unit processing.
5.Shear.General after leveling is shear.There are slitting and cut to
length. The slitting is to cut the edge or according to the width of the
need, the cut to length is according to the length of the need to be
cut into sheets.
6.Packing and delivery,after the inspection and classification of the
cold rolled steel coil coated with anti-rust oil and the packing and
delivery to the customers.